Home / Blog / Ceramic Drilling Without Chipping

Ceramic Substrate Drilling Without Edge Chipping

Ceramic Substrate Drilling · 2026-10-31 · 7 min read

Short answer: Ceramic substrates (AlN, Al2O3, SiC, ZrO2) are brittle, so chipping is a tool-and-energy problem: use diamond-coated or PCD tooling, and pick the process by hole size — laser at or below 0.15 mm, mechanical diamond-coated 0.2-0.5 mm, hybrid above 1.0 mm. Beryllia (BeO) dust is toxic and must be handled in sealed laser equipment.

Number: Polycrystalline diamond (PCD) runs at HV 8000-10000, about 5-8x the hardness of carbide, and alumina-grade tools last over 50x a carbide tool (linkuttools, tshztech). Industry chipping rates can reach 30 percent with the wrong setup but exceed 95 percent with high-speed, closed-loop control at about plus/minus 0.02 mm (engelcnc). Aperture rule of thumb: <=0.15 mm laser (10-20 ns, 50-100 kHz, HAZ <5 um), 0.2-0.5 mm mechanical diamond-coated (118-degree edge, 30k-50k rpm, 50-100 mm/min, air cooled), >1.0 mm laser plus mechanical hybrid (ipcb).

Boundary: The material set (entry/backup) only stabilizes the workpiece; the drill tool (diamond/PCD) and process own chipping control. Beryllia (BeO) is toxic — we describe sealed laser handling, not encourage mechanical machining of BeO.

Ceramic substrate PCB drilling without chipping diamond PCD tooling AlN Al2O3 SiC — YUESHAN
YUESHAN QC bench inspecting diamond-drilled ceramic substrates for edge quality.

Ceramic substrates (AlN, Al2O3, SiC, ZrO2) are used where FR4 cannot go — high thermal conductivity, low loss, dimensional stability. But they are brittle, and edge chipping at the hole is the failure mode that decides yield.

Tooling is non-negotiable: diamond or PCD

ToolPropertyWhen
PCD (polycrystalline diamond)HV 8000-10000, 5-8x carbide hardnessProduction ceramic drilling, longest life
Diamond-coated microdrillCVD diamond on carbideFine holes, M9 ceramic-filled boards
Alumina-grade toolLife >50x carbideSelected ceramic grades

Split the process by hole size

YUESHAN supplies the stable aluminum entry and rigid backup used to hold ceramic substrates flat during drilling; the diamond/PCD tool and process own chipping control. See the ceramic drill-bit selection and bit-life ceramic vs FR4 pages for tool detail.
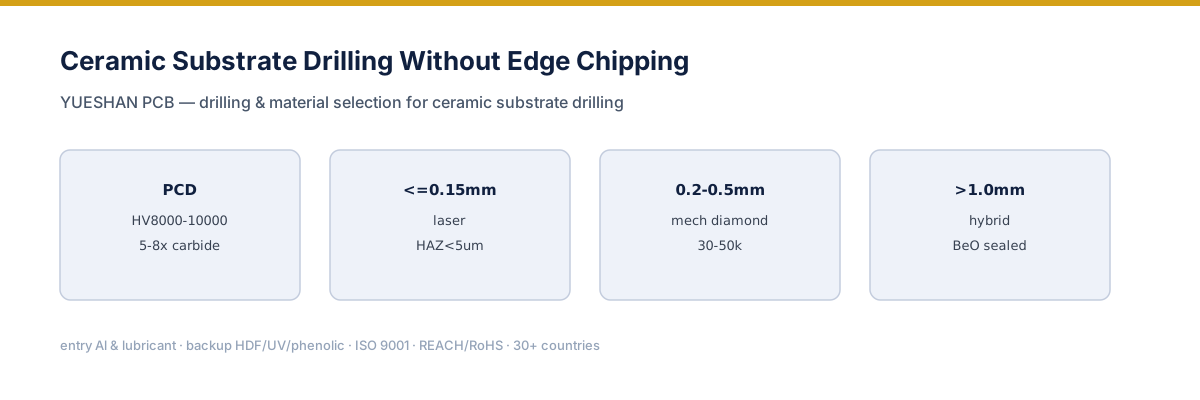
Ceramic drilling no-chipping process diagram
Tool hardness and the aperture-based process split.
Entry">Al rigid

Aluminum Entry

flat, stable clamp

entry →
Backup">Phenolic

Phenolic Backup

rigid support

phenolic →
Tool">Diamond

Ceramic Drill Selection

PCD vs CVD diamond

tool →
Pillar">Drilling

Mastering PCB Drilling

process + material map

pillar →
← Back to Blog Request Free Samples →

Frequently Asked Questions

YUESHAN supplies the stable aluminum entry and rigid backup used to hold ceramic substrates (AlN, Al2O3, SiC, ZrO2) flat during drilling. The questions below cover tooling and the process split by hole size.

Why does ceramic substrate drilling chip at the edge?

Ceramics are brittle, so chipping is a tool-and-energy problem — the wrong tool or too much mechanical stress at the edge. Industry rates can reach 30 percent chipping but exceed 95 percent with high-speed, closed-loop control at about plus/minus 0.02 mm (engelcnc).

What tool do you use for ceramic PCB drilling?

Diamond or PCD is mandatory: PCD runs at HV 8000-10000, about 5-8x carbide hardness, and alumina-grade tools last over 50x a carbide tool (linkuttools, tshztech).

When do you use laser versus mechanical drilling for ceramic?

At or below 0.15 mm use laser (10-20 ns, 50-100 kHz, HAZ less than 5 um); 0.2-0.5 mm uses mechanical diamond-coated (118-degree edge, 30k-50k rpm); above 1.0 mm uses a laser plus mechanical hybrid (ipcb).

Can you drill beryllia (BeO) ceramic?

BeO dust is toxic, so it must be handled only in sealed laser equipment; we describe that route rather than encourage open mechanical machining (ipcb).

Does the backup board stop ceramic chipping?

The board stabilizes the substrate but does not own chipping — the diamond/PCD tool and process do. A flat, rigid backup still protects edge quality during the run.

Do you supply ceramic drilling consumables?

YUESHAN supplies the aluminum entry and phenolic/HDF backup that hold ceramic substrates flat; the diamond/PCD tool is selected by the fabricator. Request a sample to trial.

LX

Mr. Lucky Xu — Director, YUESHAN PCB — Director, YUESHAN PCB

15 years in PCB drilling consumables. Wrote and technically reviewed this page; where a number is stated, the page says how it was measured, and any third-party or industry reference (IPC, Rogers, ISO, FDA, PCD tooling, CO2/UV laser, jiepei, hilelectronic, linkut) is named inline rather than presented as a YUESHAN specification.

About the author · Editorial standards & review process · Request TDS / SDS or a sample